One clamping fewer on the same part — and the plan shows why.
MEKLYRA plans a part twice: once with coolant-driven devices in the tool list — a coolant-driven 90° head and a jet spindle — once without, and lays the two real plans side by side. Below is our demo part MEK-DEMO-07 on a 3-axis vertical machining centre in aluminium 6061-T6.
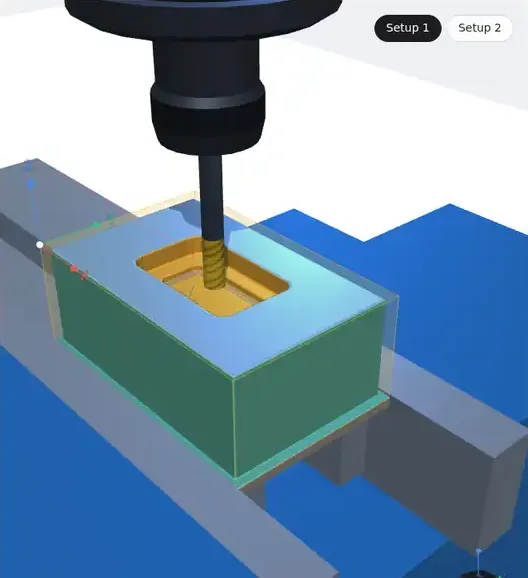
| Without | With the devices | Difference | |
|---|---|---|---|
| Clampings | 3 | 2 | −1 |
| Operations | 16 | 13 | −3 |
| Cutting tools | 6 | 6 | same |
| Cutting time per piece | 3:10 | 2:31 | −0:40 |
| Non-cutting per piece | 1:00 | 0:53 | −0:07 |
| Inspection per piece | 1:30 | 1:00 | −0:30 |
| Per piece | 5:40 | 4:24 | −1:16 |
On a batch of 100 that is about 2 h 07 min of machine time — and one fixture setup fewer, which is not in these figures.
What the devices do on this part
drills the two Ø2 side holes from the top, in setup 1. The side of the part never faces the spindle, so the third clamping disappears.
engraves the letter M with a Ø2 cutter at the spindle’s own speed, driven by the coolant pressure — the machine’s 8,100 rpm would starve a cutter that small.
Device figures come from the device maker's published catalogue.
On your own part
- Open the part in MEKLYRA — STEP model and the drawing.
- Under the plan’s times, tap Setup Saver. The part is planned a second time without the devices.
- Read the two plans side by side, and print one page for the shop.
What the numbers are — and are not
- Both columns come from the same planner, on the same model, drawing, machine, material and stock. The only difference is whether the coolant-driven devices are in the tool list. Nothing is estimated for the comparison.
- Times use the machine record and the shop’s own load and tool-change times. The one-off fixture setup per batch is not counted, so a clamping saved is worth more than the table shows.
- When a device changes nothing on a part, MEKLYRA says so plainly — not every part needs one.
Numbers from MEKLYRA build 447, 23 September 2026.